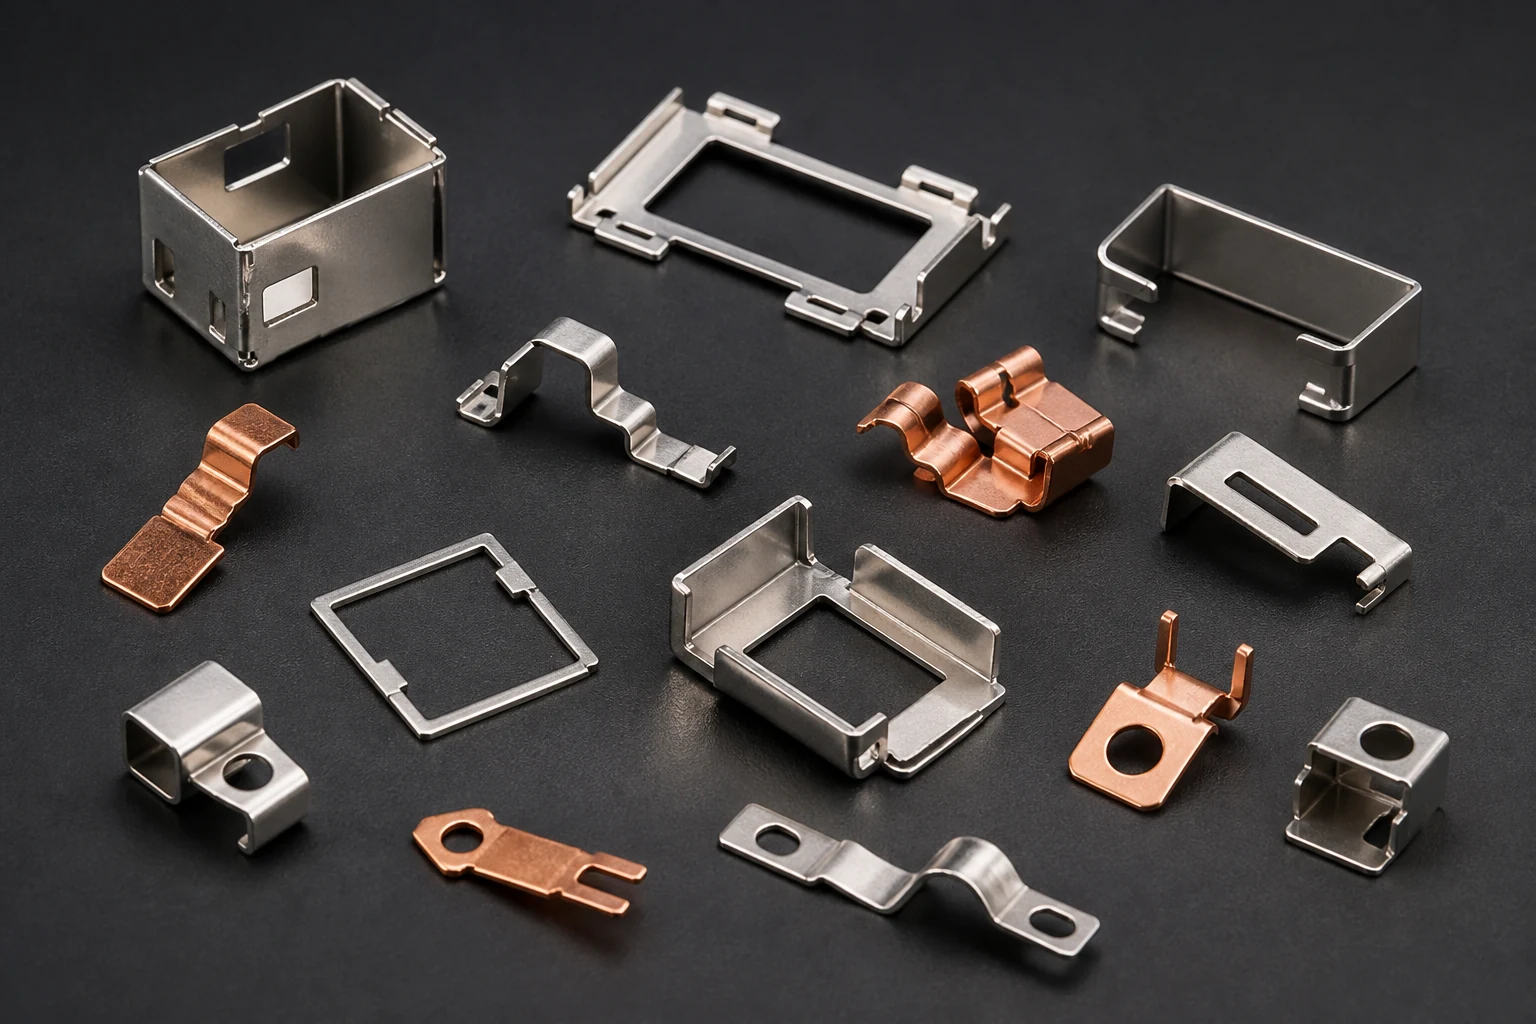
Plating acceptance on stamped terminals should separate coating adhesion from coating thickness. ASTM B571-23 selects qualitative adhesion tests based on intended use and calls for the method to be identified in acceptance inspection. ASTM B568 and B487 provide X-ray spectrometry and cross-section microscopy routes for thickness measurement. A thickness reading does not prove adhesion.
Record the manufacturing steps experienced by the coating
Identify substrate and temper, pretreatment, coating sequence, target layer thicknesses, stamping and bending sequence, solder reflow or post-treatment. Preplated strip and post-plated formed parts can have different inspection locations and edge-coverage conditions. Mark functional faces, sheared edges and high-strain areas on the process drawing.
A coupon is comparable only when its material, surface state and plating route represent the production part. ASTM B571-23 allows an agreed representative panel when component size or shape prevents a direct test and describes using the same material, surface finish and plating cycle as the represented part.
Choose adhesion tests that represent downstream use
ASTM B571-23 identifies bend or draw methods as candidates for articles that will be formed and heat-quench methods for articles that will be soldered or otherwise heated. Each method has restrictions by substrate, coating, thickness and ductility, so select it for the actual material and process sequence.
The acceptance document should state magnification, criteria for peeling or blistering, sampling location and boundary-sample rules. Parties should agree on interpretation before results fall near the limit of a qualitative method.
Select thickness methods for the geometry and question
ASTM B568 uses X-ray spectrometry for non-destructive measurement on suitable material combinations. Measurement volume, curvature and substrate affect the result. ASTM B487 measures a prepared cross-section by microscopy, revealing local layers but requiring sectioning and preparation. Define calibration, locations and units for either method.
A flat witness coupon average does not automatically represent a sheared edge, hole wall or bend inside radius. For critical locations, evaluate a functional part or an agreed same-process specimen and determine whether process changes invalidate prior evidence.
- Identify the substrate, each coating, total thickness and critical measurement zones
- Select adhesion methods for forming, soldering and heat exposure after plating
- Report specimen representativeness, lot, inspection conditions and acceptance rule
Use process changes to trigger a coverage review
Changes to substrate, pretreatment, plating bath, thickness, forming sequence or reflow conditions may affect the validation coverage. Keep first-article cross-sections, functional parts and lot records so supplier changes can be compared against existing evidence.
Apply this guide to a project
Use product pages to identify the hardware family and the calculator for early estimates only. Acceptance depends on drawings, operating conditions and project tests.